Chemical storage requires more than high-density racking. Flammable, explosive, corrosive, toxic, and other hazardous materials have different storage characteristics and segregation requirements, while temperature, humidity, leakage prevention, ventilation, and access control may also need to be carefully managed.
Zhuku provides chemical warehouse storage solutions that combine high-density automated storage, controlled storage zones, automated material handling, environmental monitoring, and warehouse software to reduce unnecessary human exposure and improve the safety, visibility, and consistency of chemical warehouse operations.
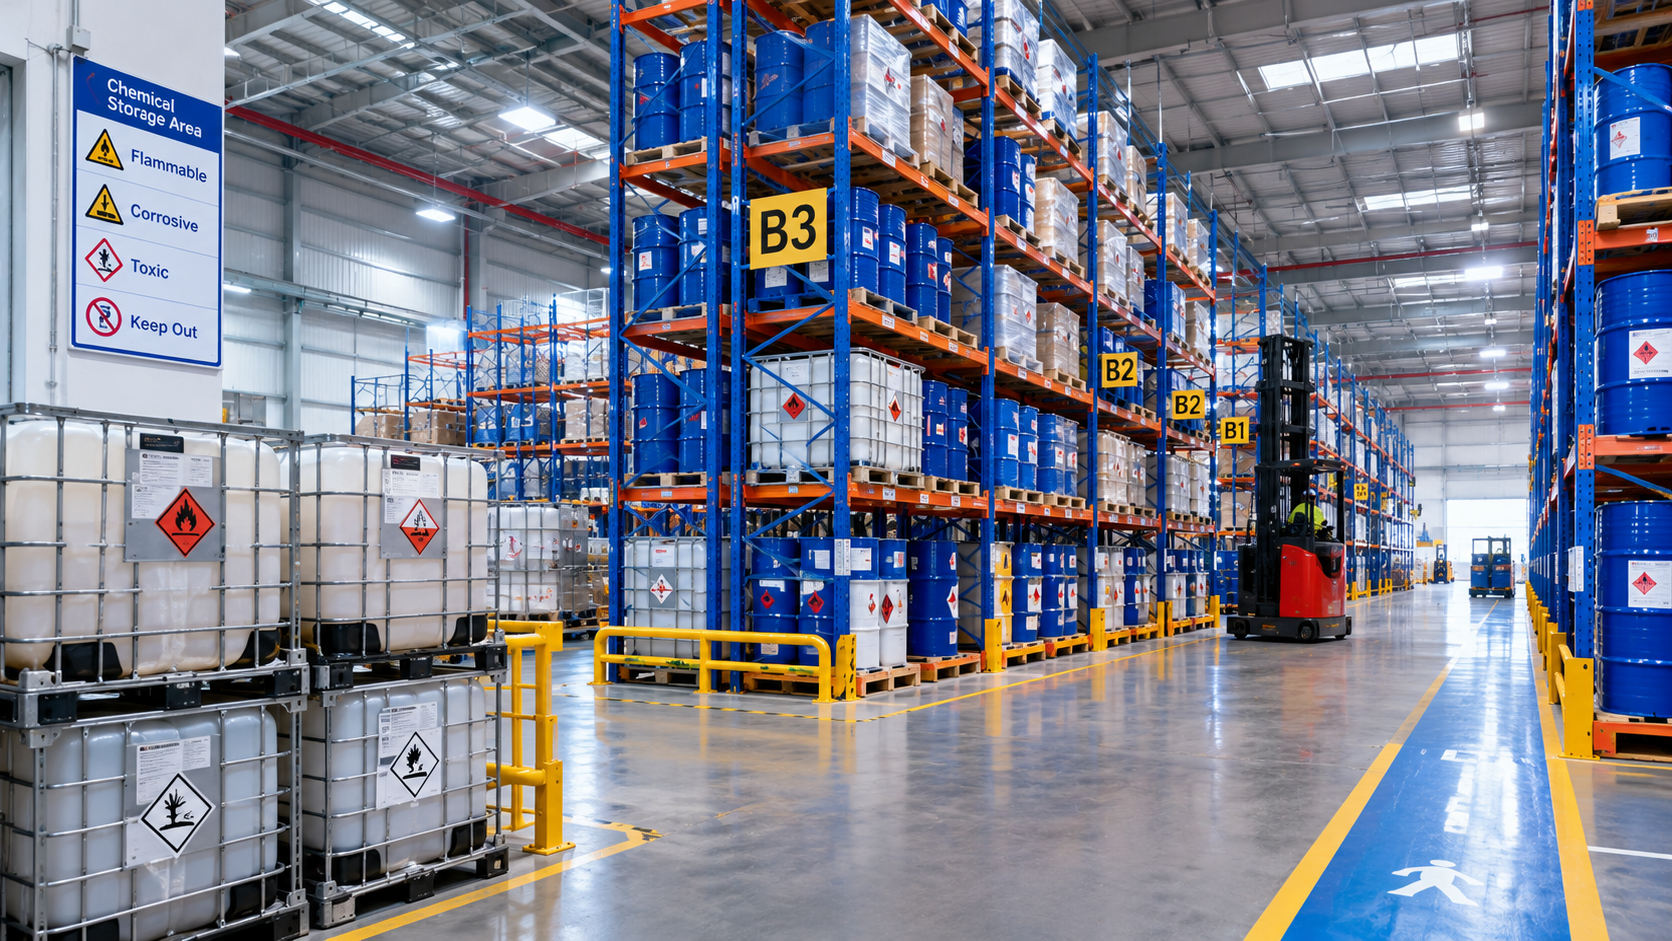
Chemical warehouses often need to manage multiple risks at the same time. Zhuku designs the automation system around the actual chemical characteristics, warehouse environment, storage capacity, and operational requirements.
Hazardous Materials Require Strict SegregationDifferent chemicals cannot simply be stored together Flammable, explosive, corrosive, and other chemical products may have different compatibility and segregation requirements. Clearly defined storage zones help prevent inappropriate co-storage and simplify warehouse management. |
Manual Handling Creates Additional Safety RisksReduce unnecessary personnel exposure Frequent manual storage and retrieval can increase worker exposure to hazardous materials. Automated handling can move products through predefined workflows with less routine personnel intervention. |
Environmental Conditions Must Be ControlledMaintain a stable storage environment Some chemical products require controlled temperature, humidity, ventilation, sealing, or leakage-prevention measures. Manual inspection alone may not provide continuous visibility. |
Inventory Requires Accurate TraceabilityKnow exactly what is stored and where Chemical warehouses need reliable information about product type, quantity, batch, location, storage status, and movement history. |
High Storage Density Can Be Difficult to AchieveUse warehouse space more efficiently Large quantities of chemical products can require significant storage capacity. High-density pallet storage and automated retrieval can help maximize usable warehouse space. |
Operations Must Remain Consistent Around the ClockAutomate repetitive storage activities Automated equipment and warehouse software can execute standardized putaway, storage, retrieval, and inventory processes with reduced dependence on manual operations. |
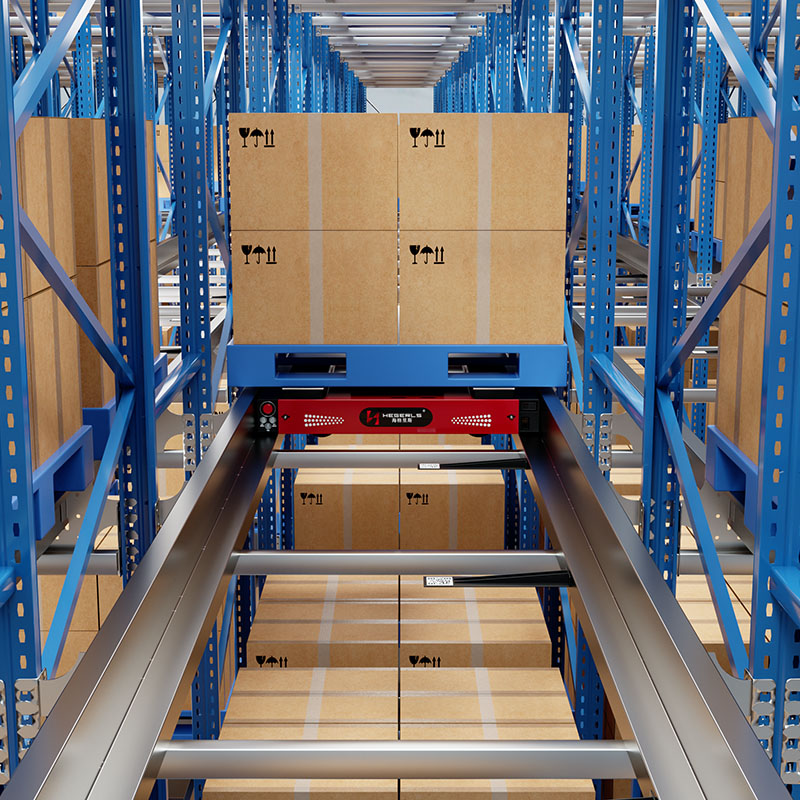
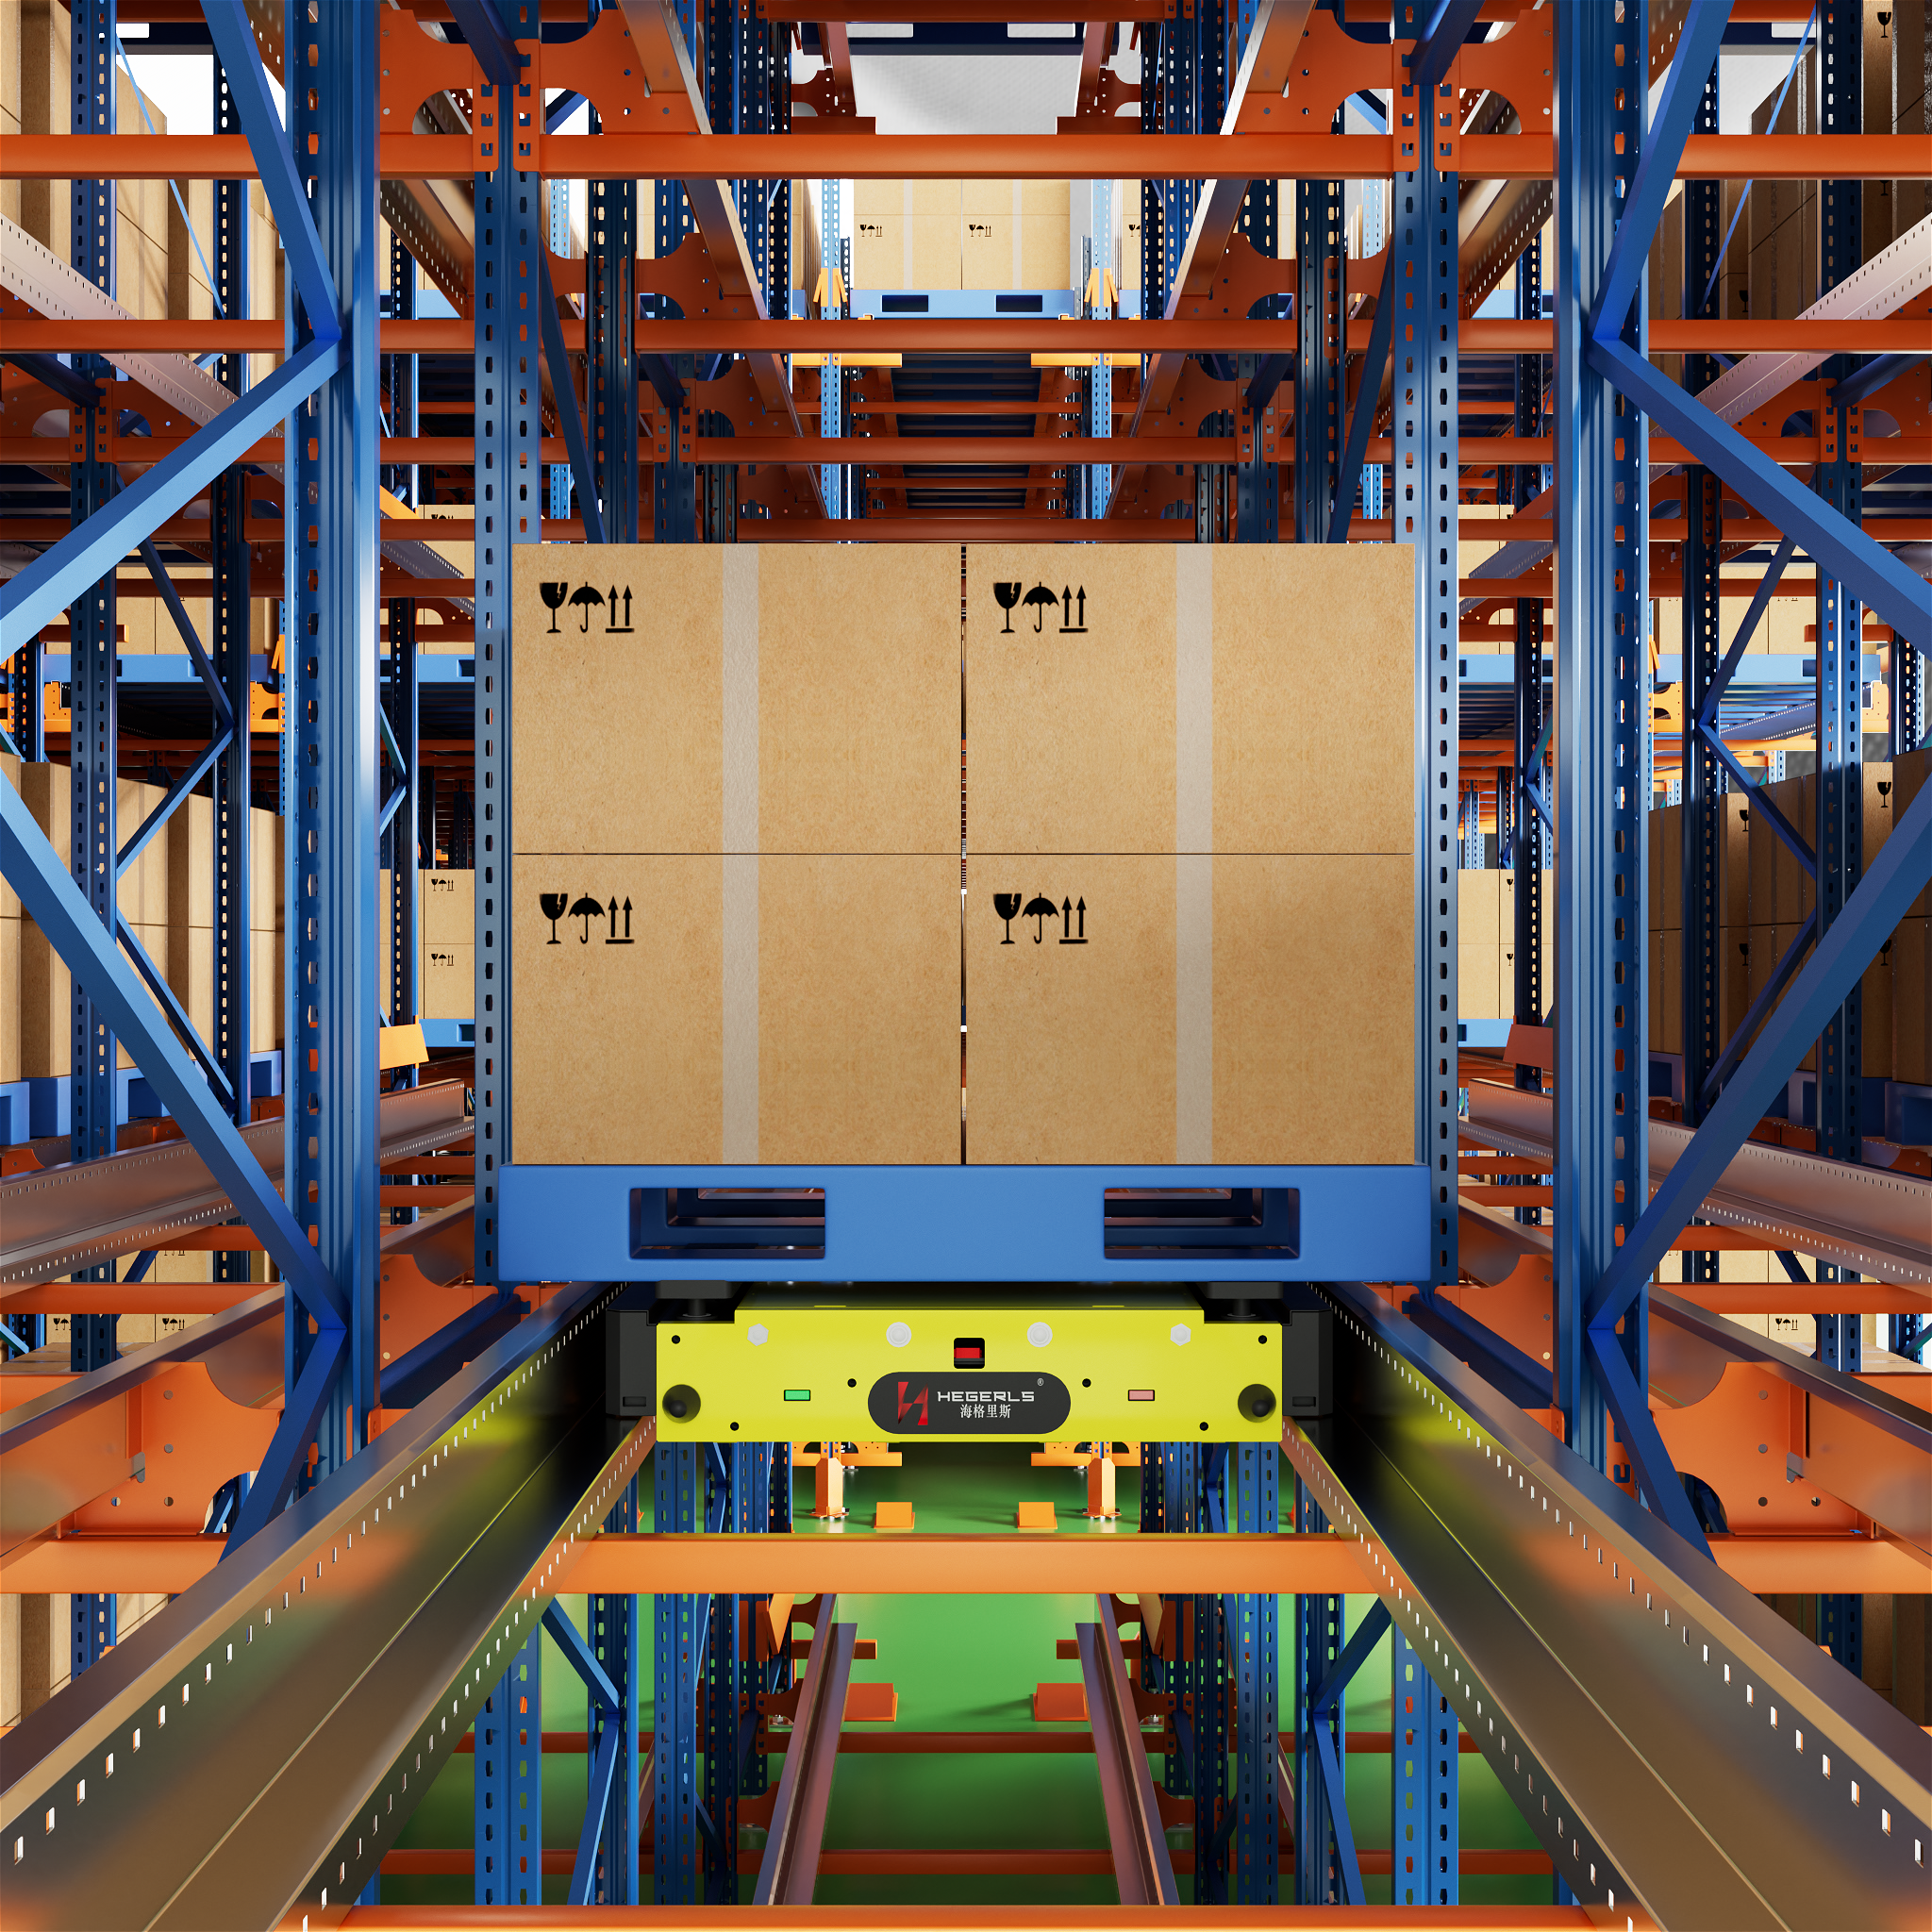
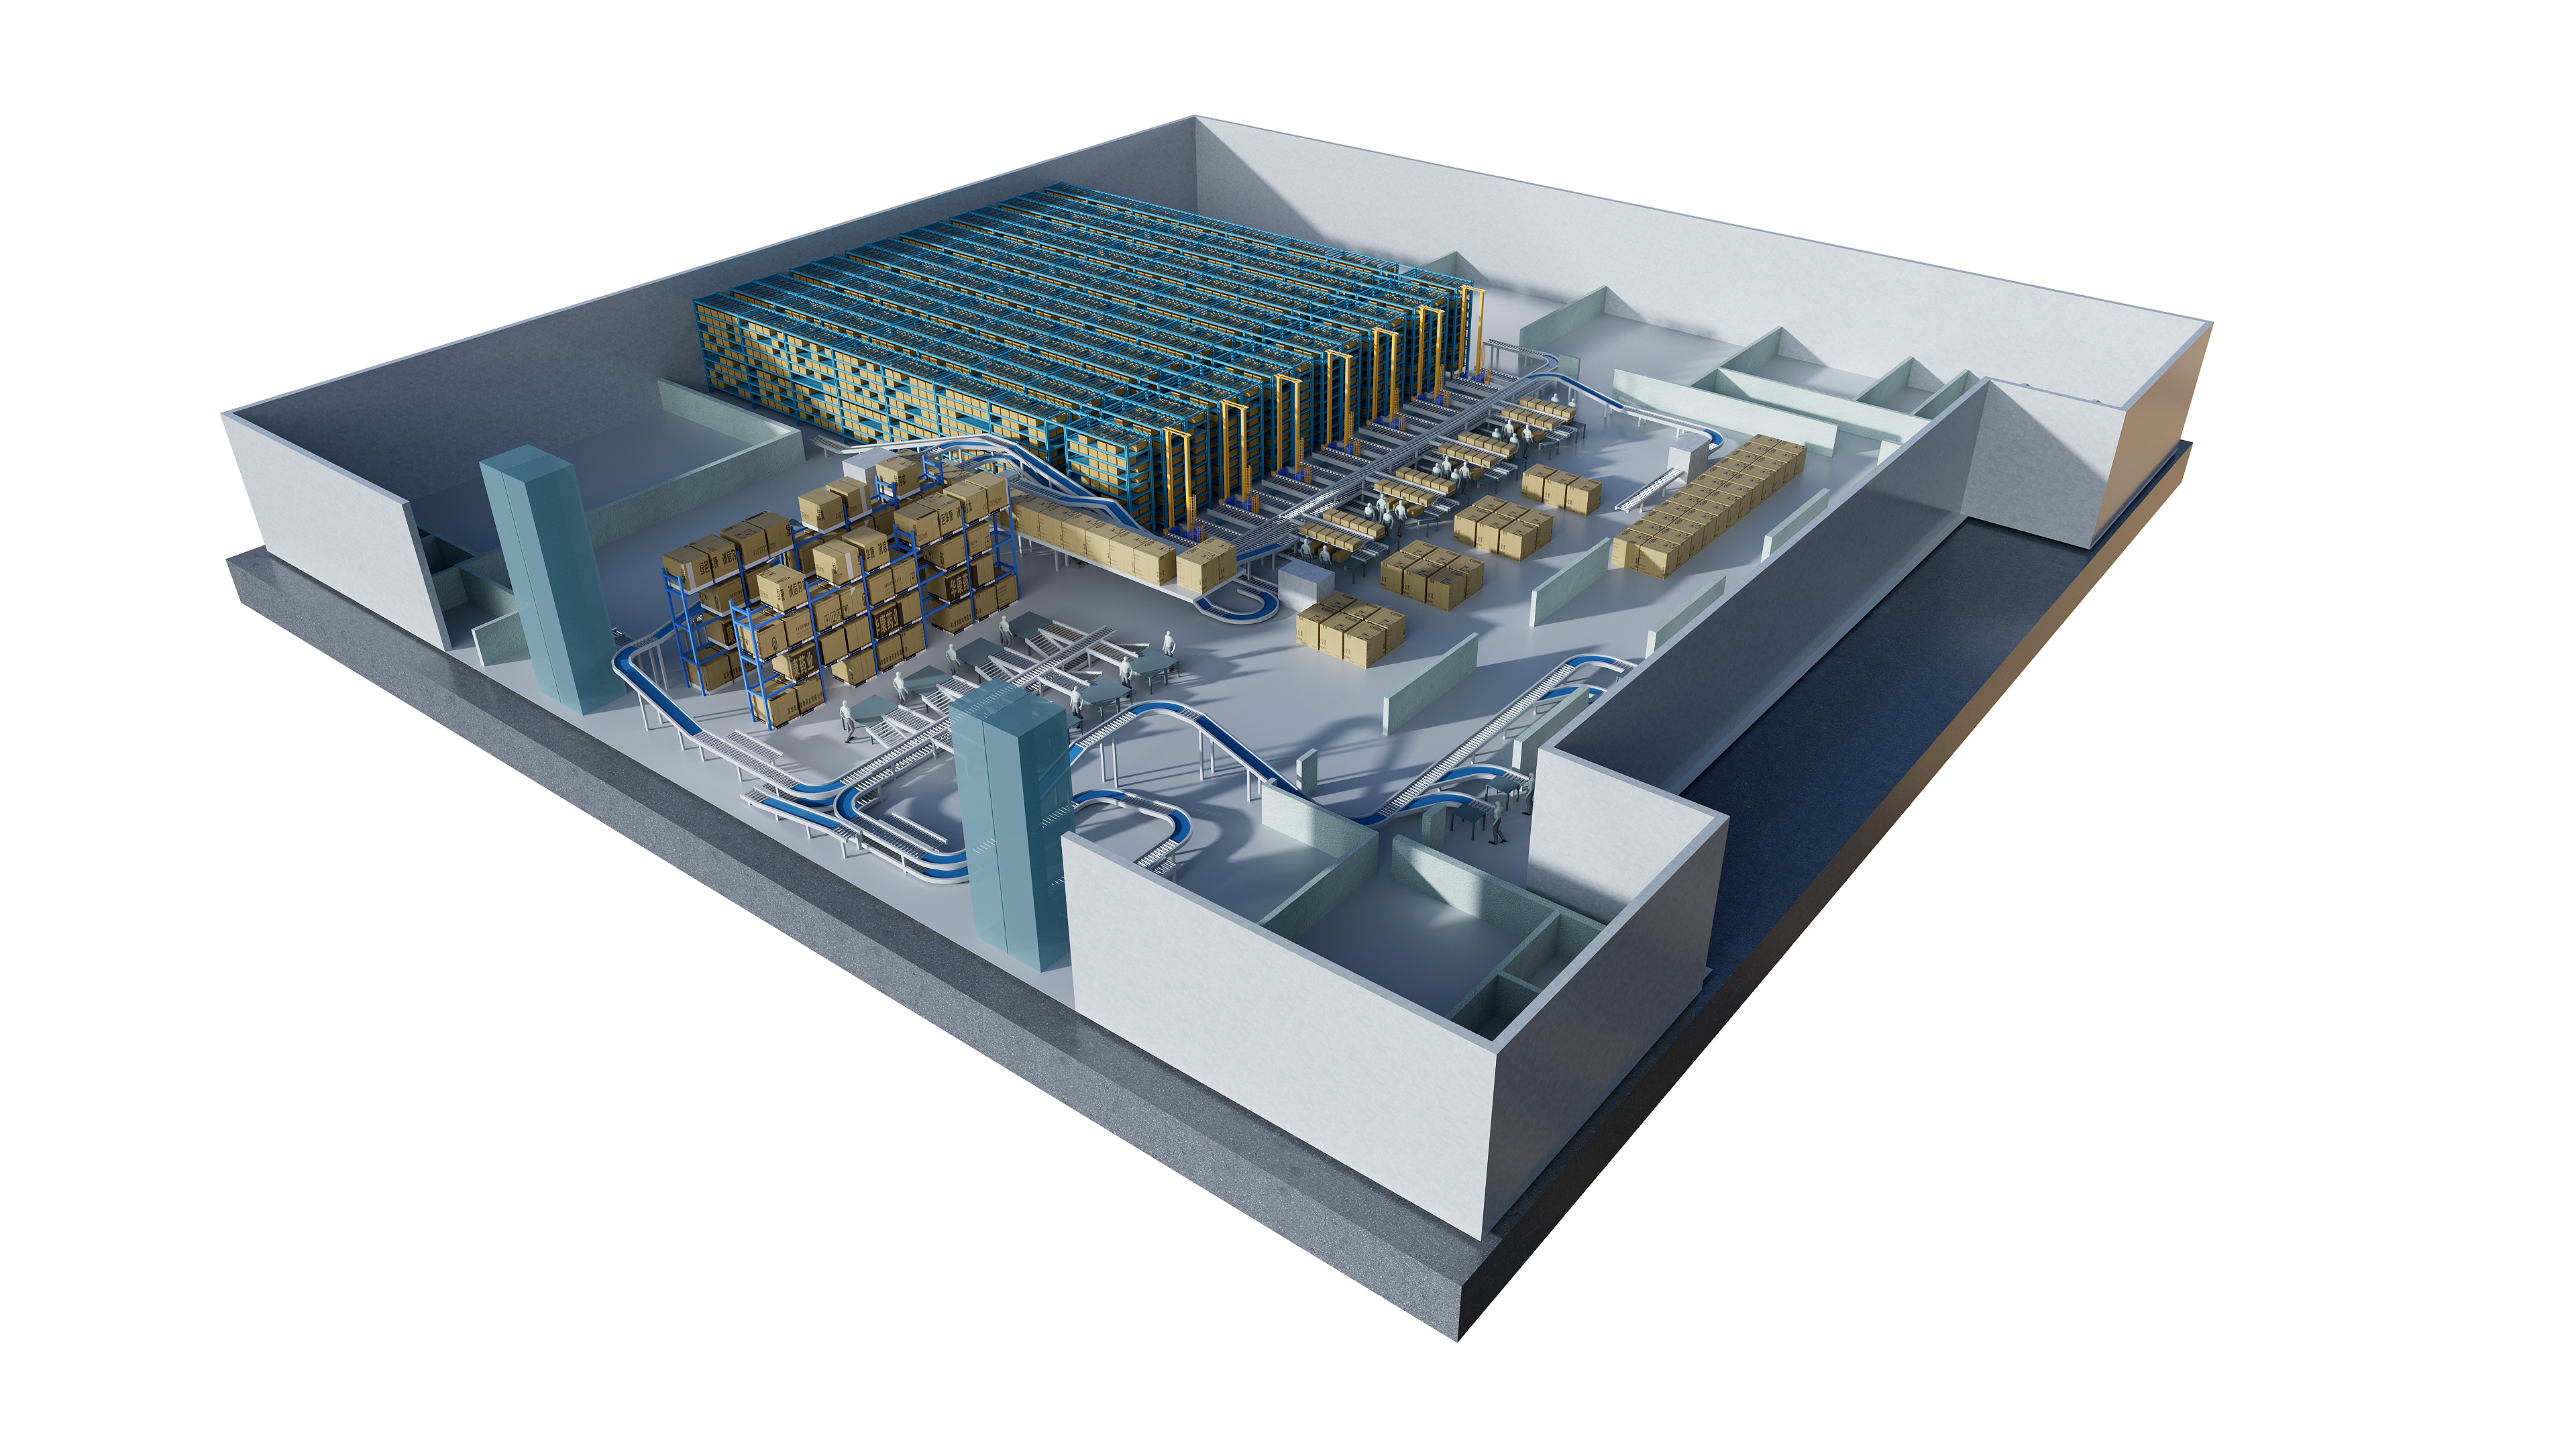
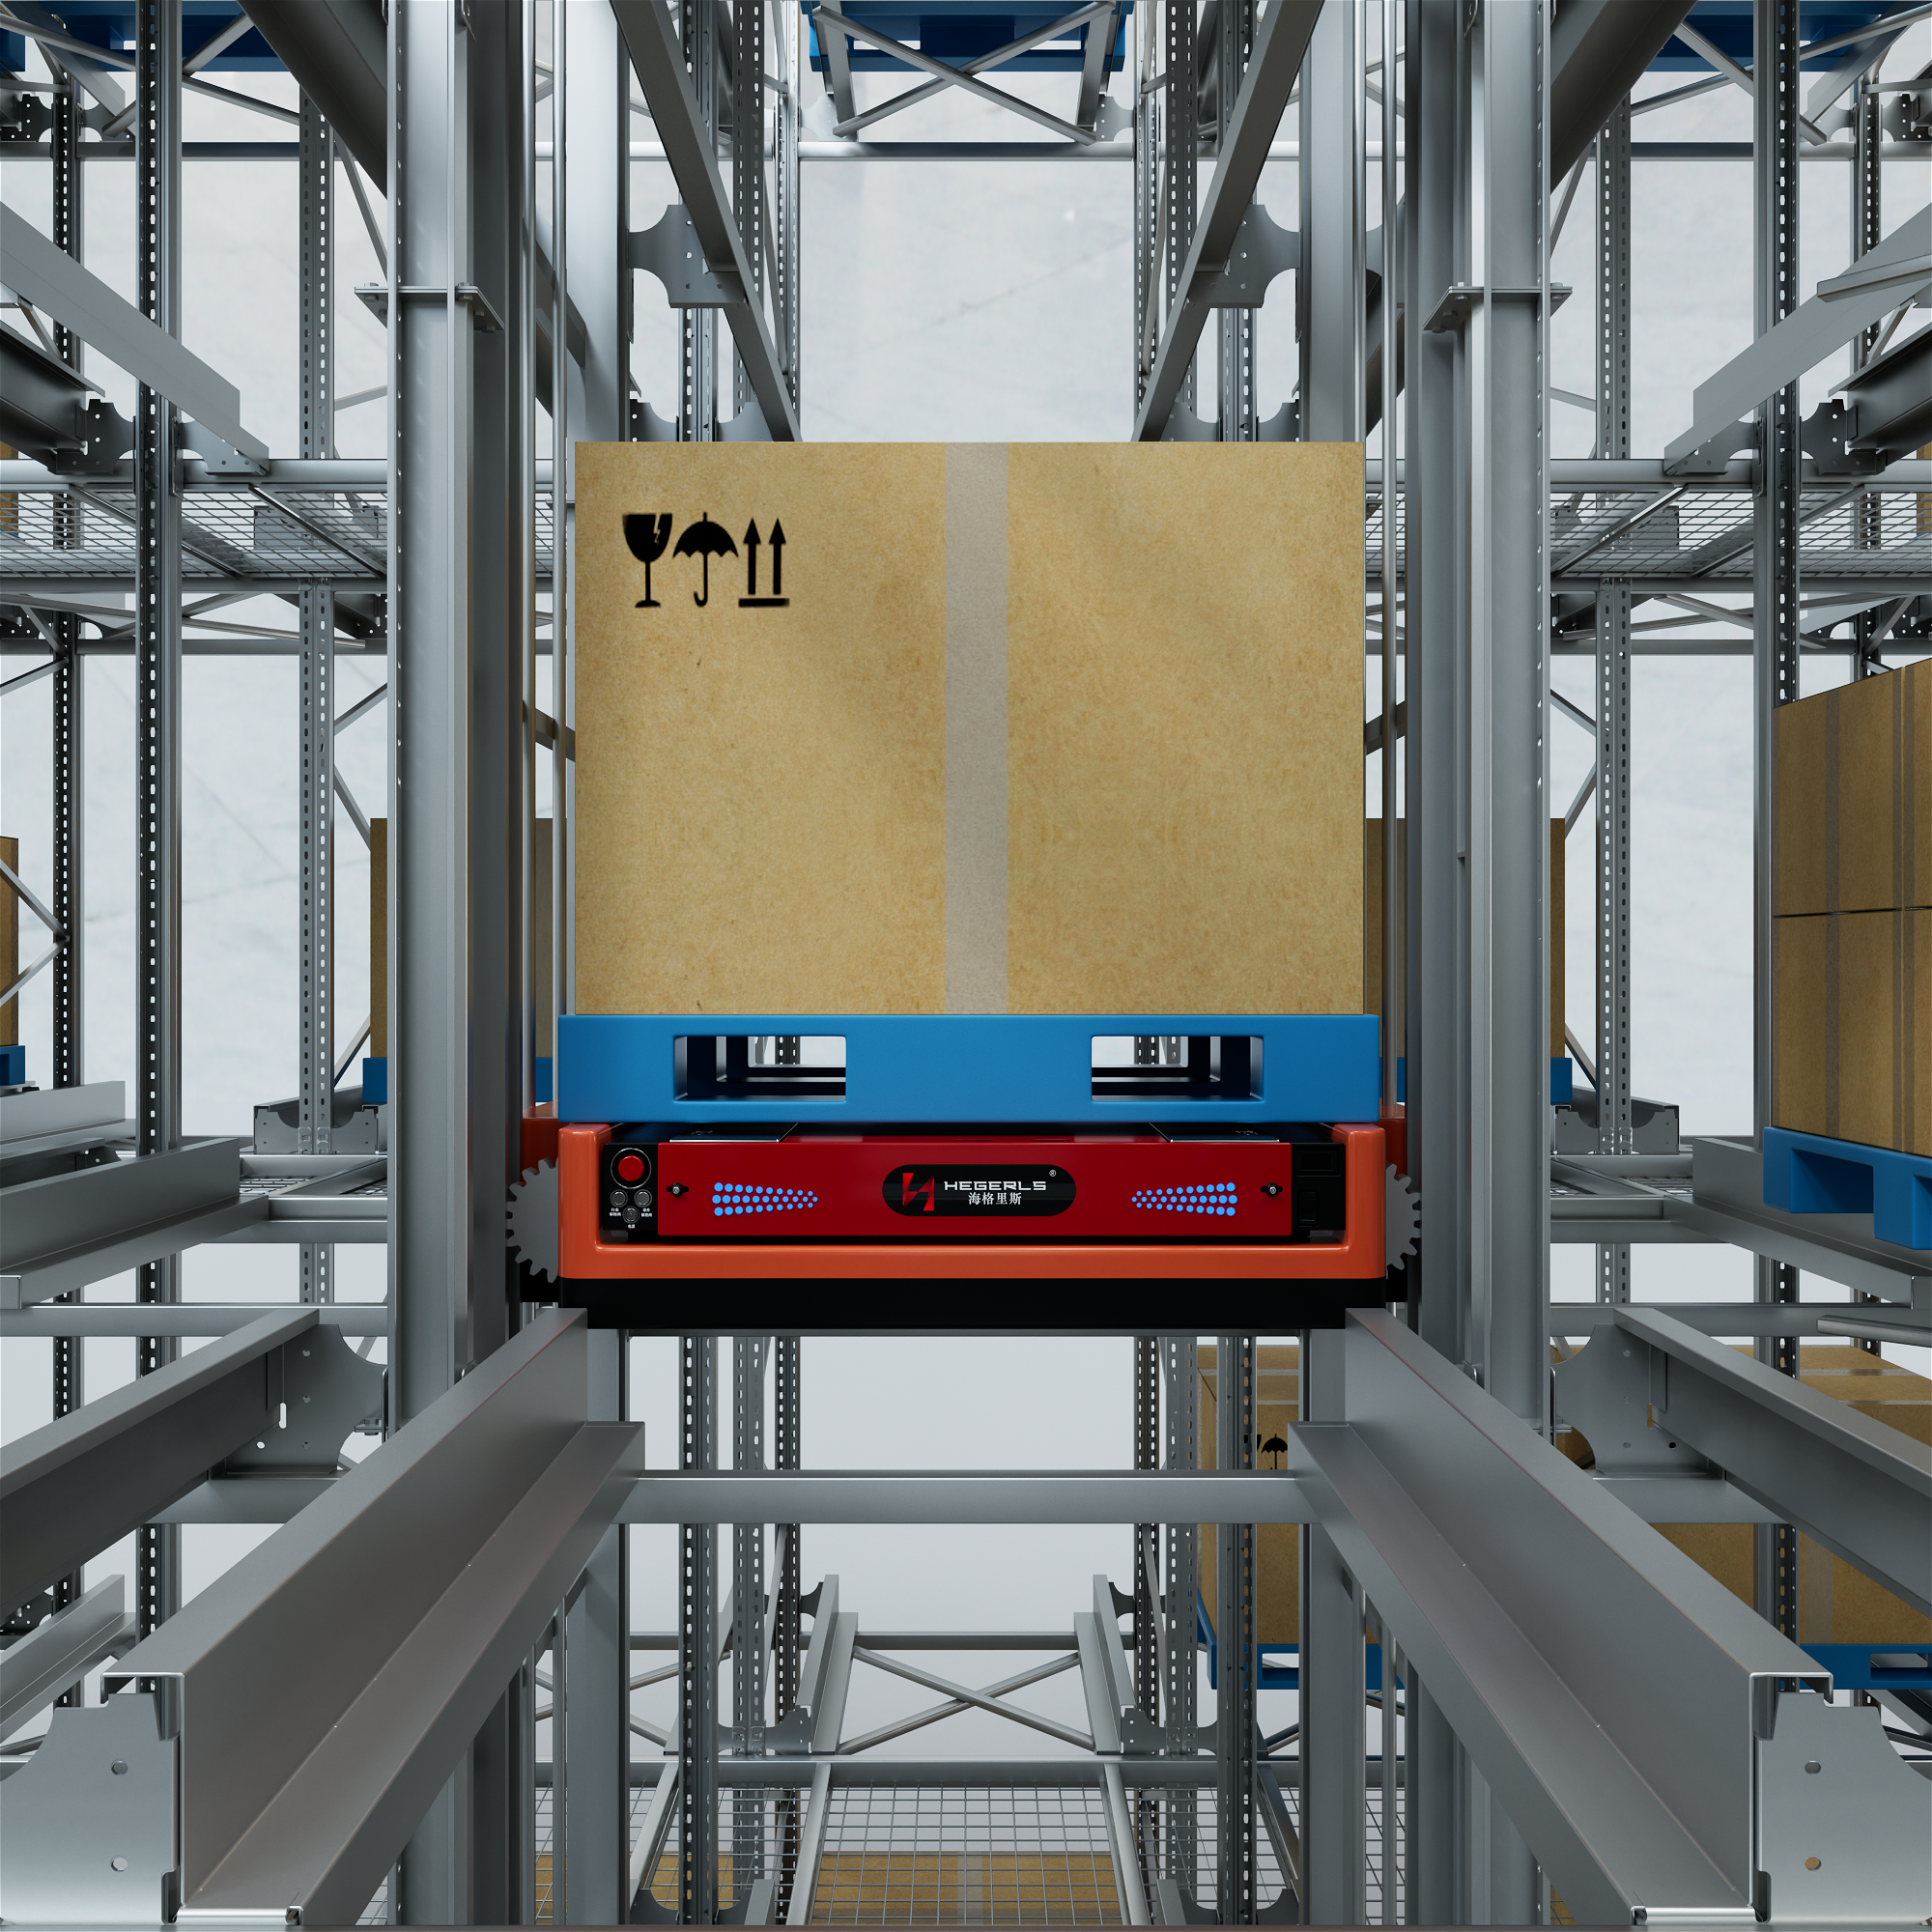
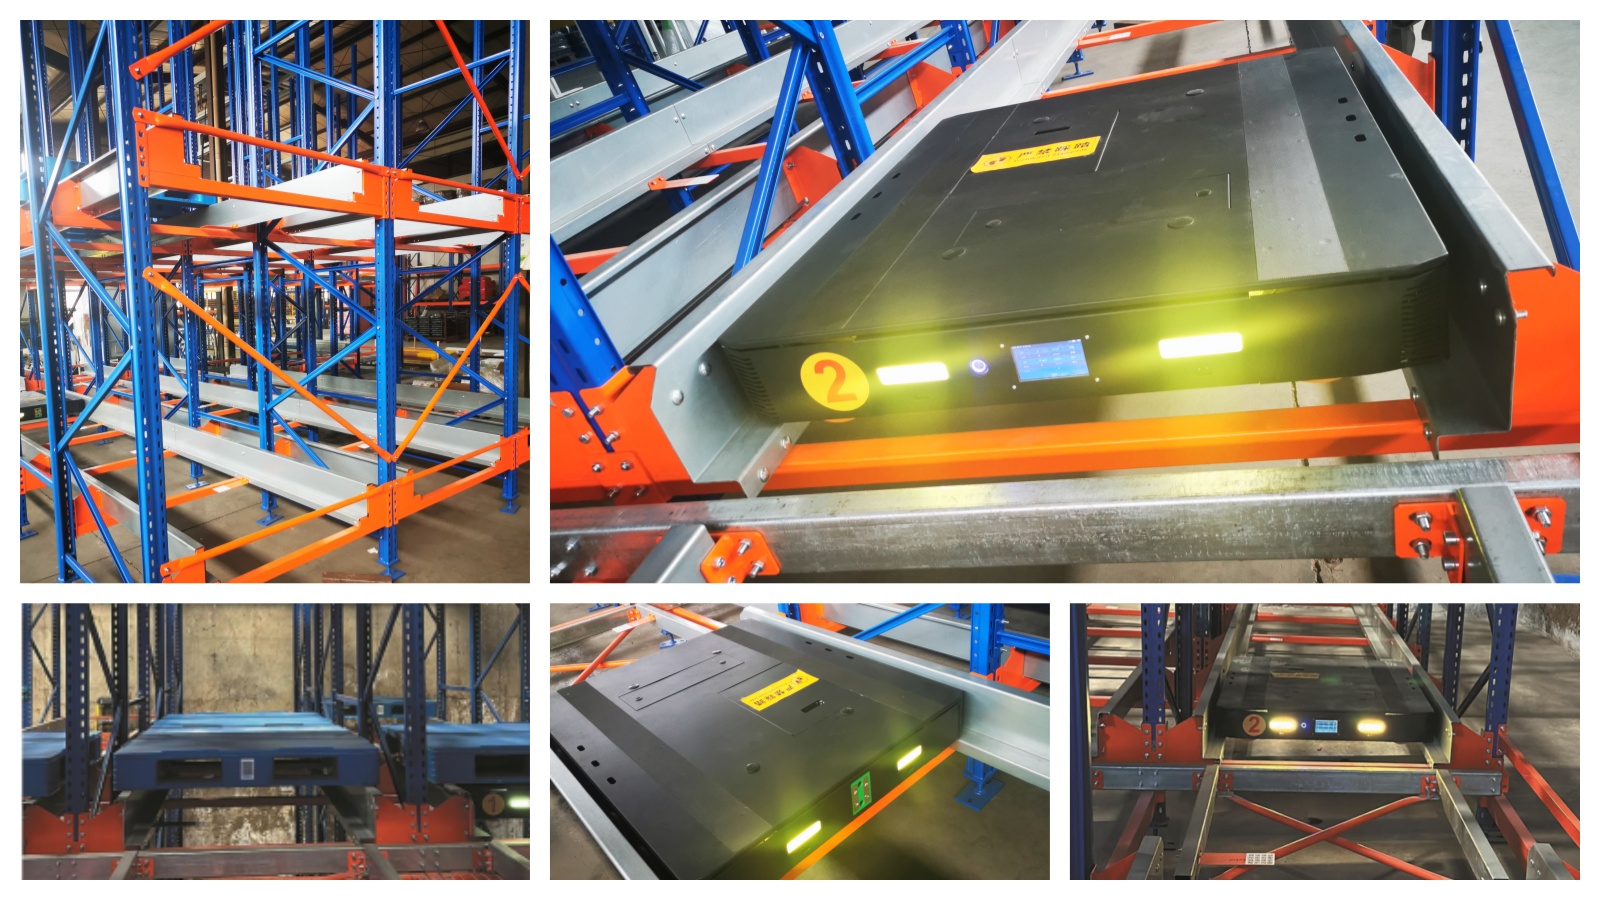
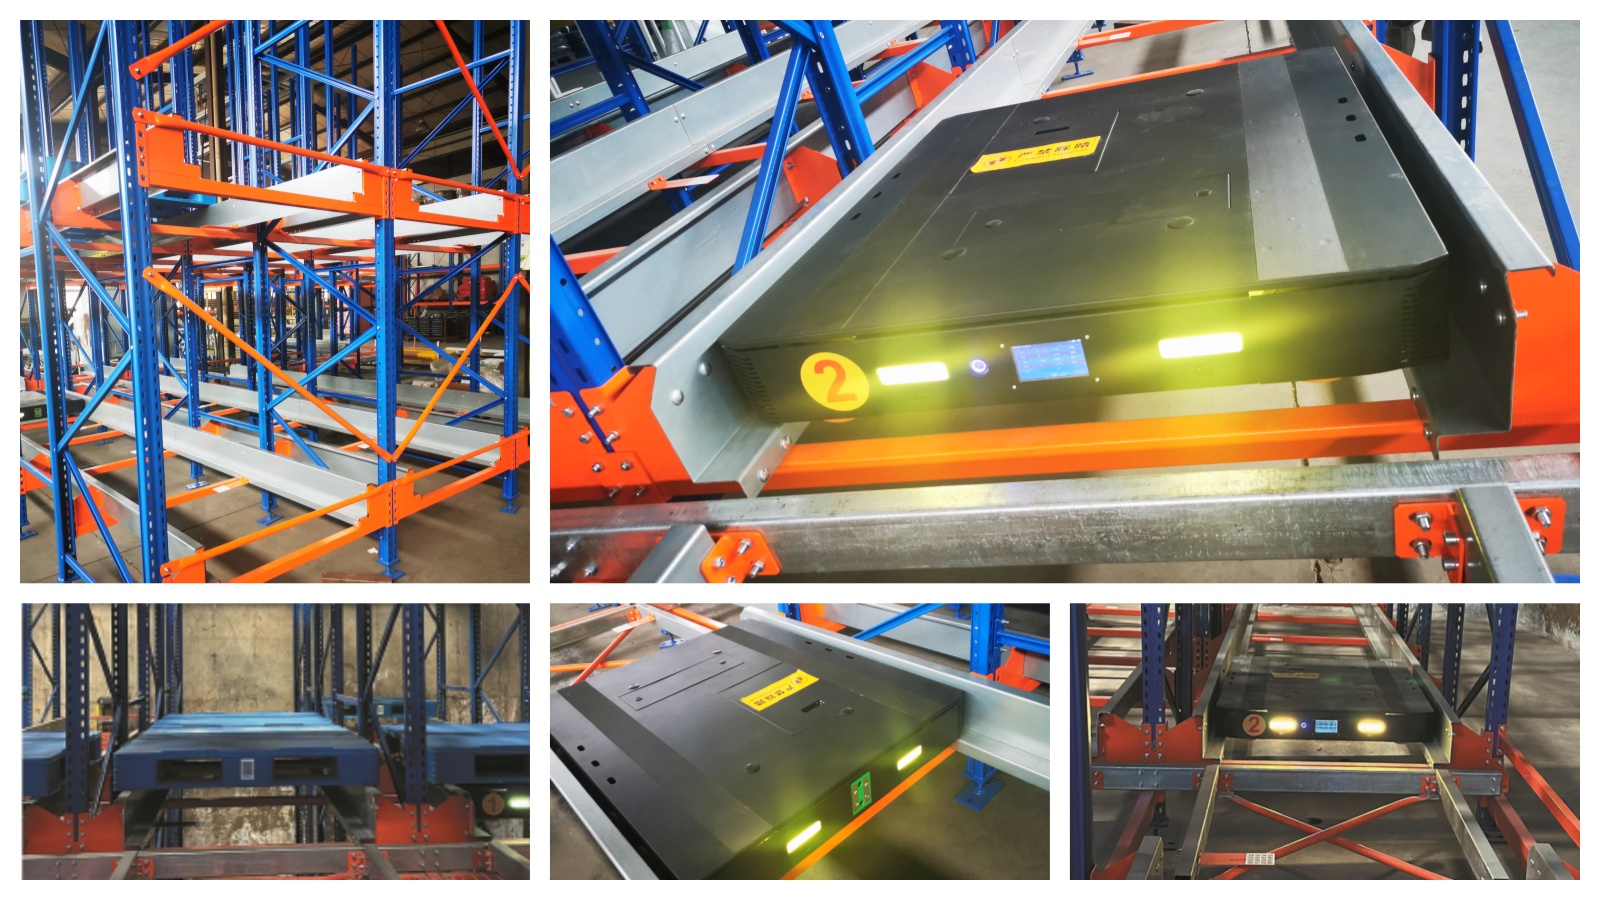
1. Classified & Segregated StorageDedicated zones for different chemical requirements Zhuku designs storage locations according to chemical characteristics, compatibility, hazard classification, packaging, environmental requirements, and operational workflows. 2. Automated High-Density StorageStore more pallets within controlled areas Four-way shuttle systems, pallet shuttle systems, and stacker crane ASRS can be selected according to storage density, warehouse height, pallet specifications, and throughput requirements. 3. Explosion-Protected ConfigurationEquipment designed for the required hazardous environment Where required, storage and material-handling equipment can be configured according to the project's hazardous-area classification and applicable technical requirements. 4. Automated Material HandlingReduce unnecessary manual movement Conveyors, lifts, shuttles, and stacker cranes connect receiving, storage, retrieval, and dispatch processes through controlled automated workflows. |
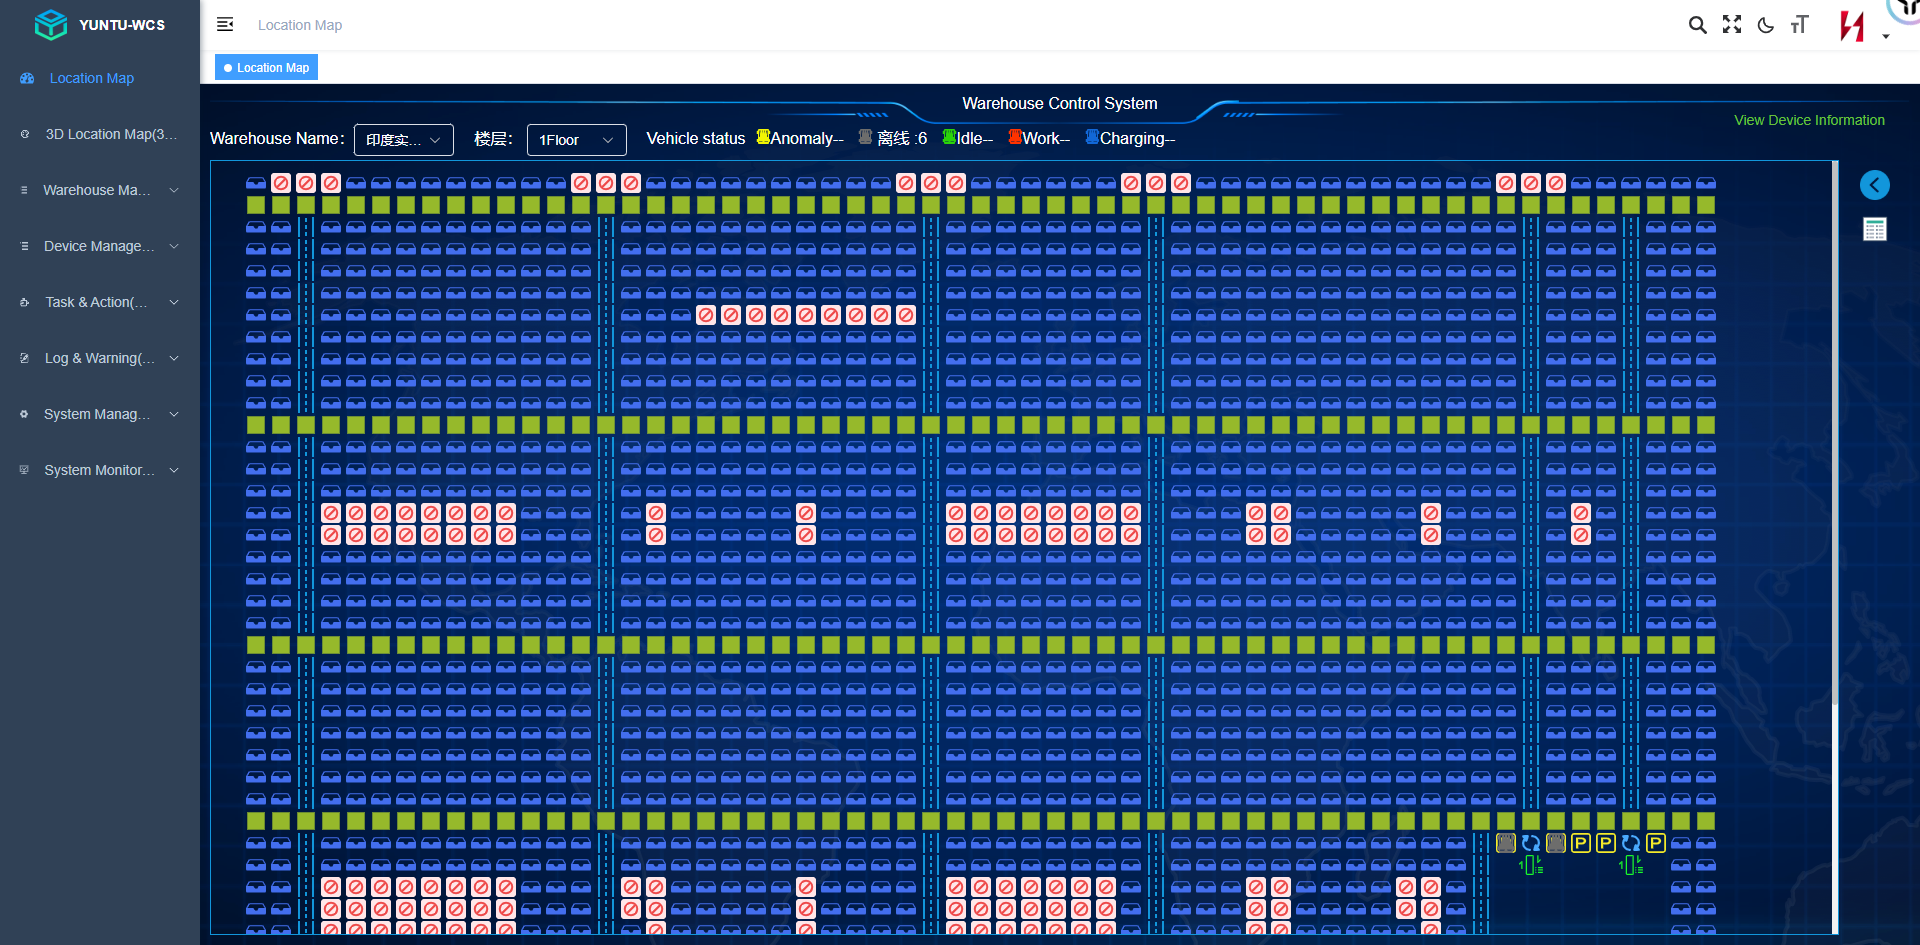
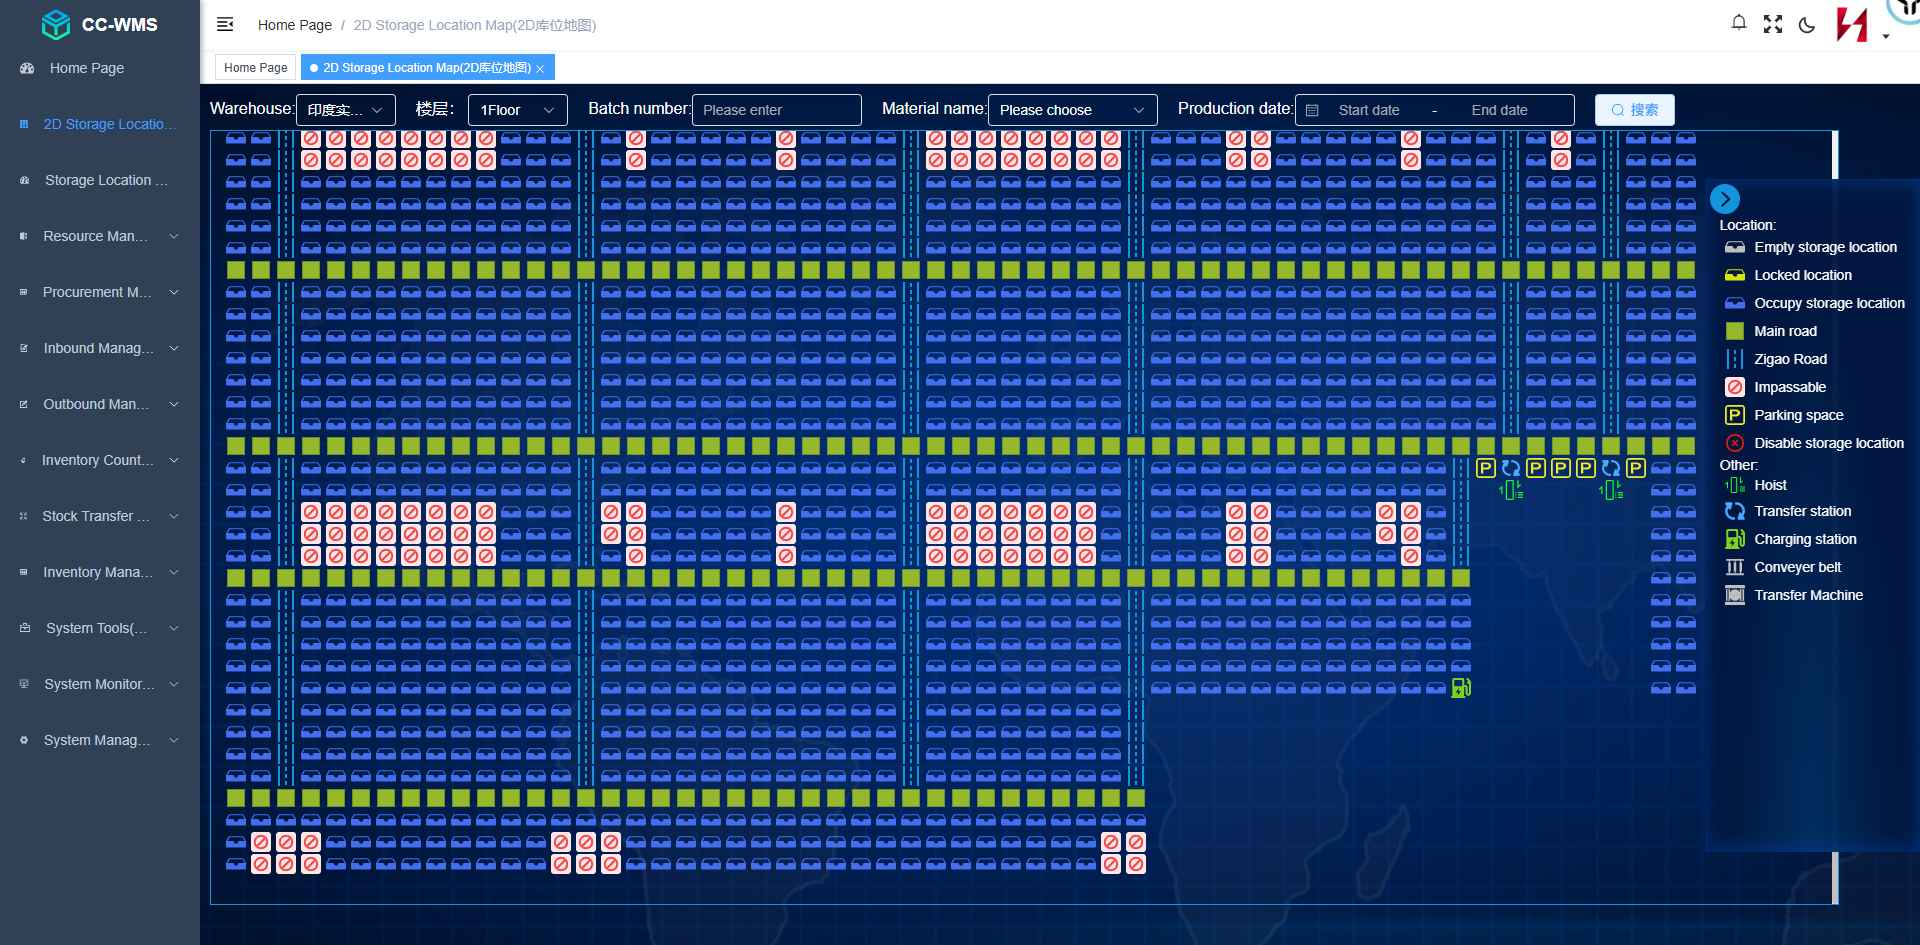
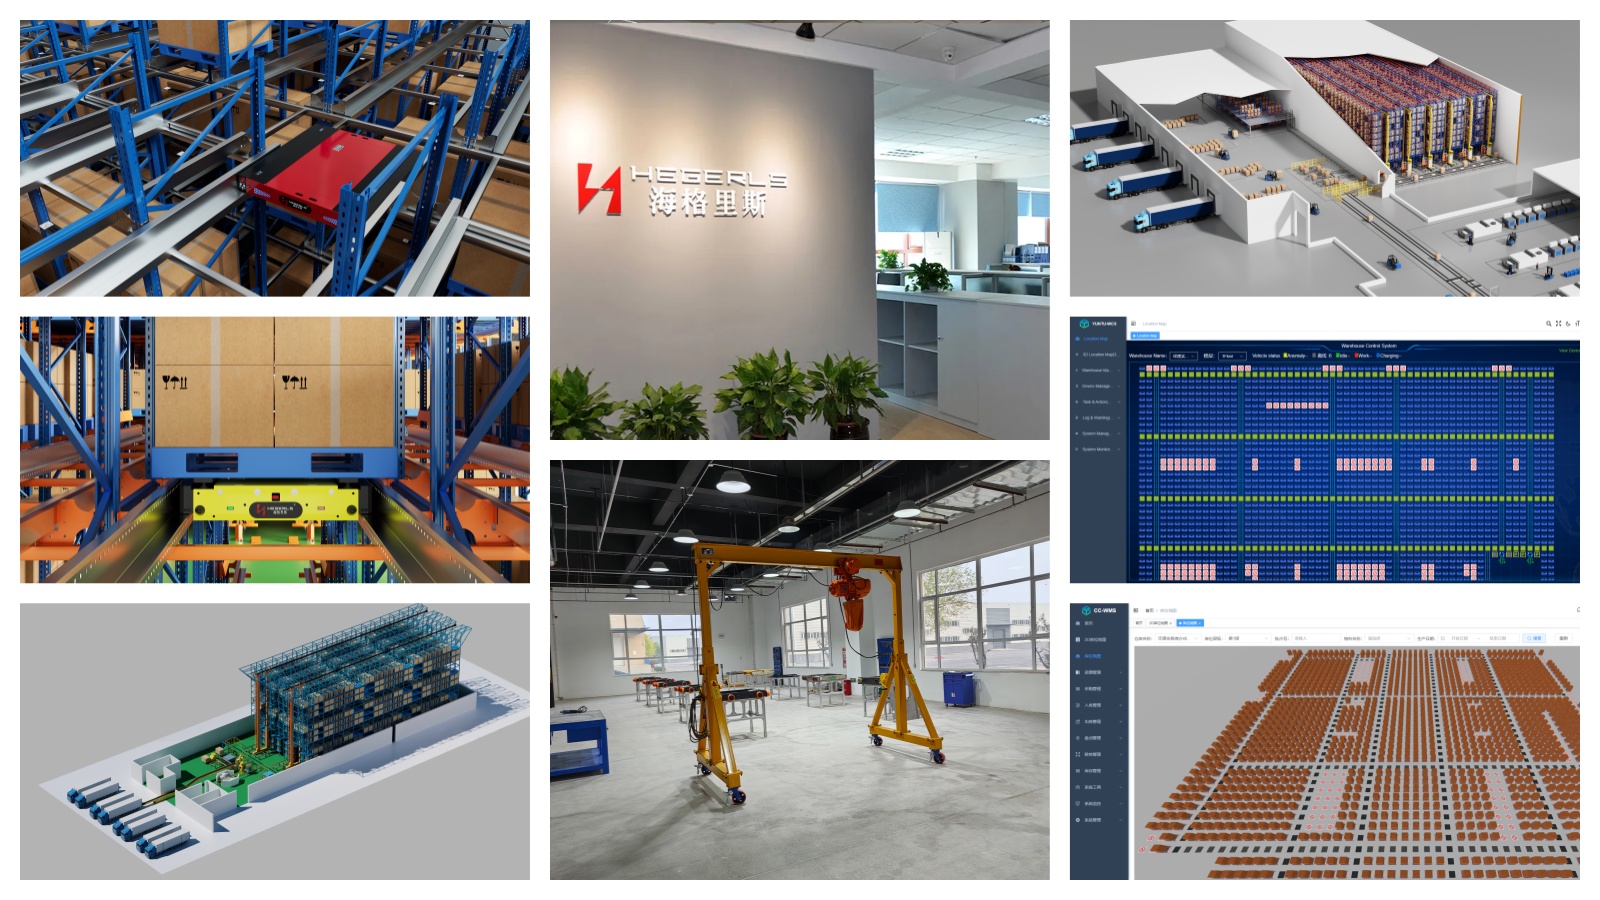
5. Environmental MonitoringTrack critical warehouse conditions continuously Sensors and monitoring systems can be integrated to monitor temperature, humidity, and other project-specific environmental parameters, with alerts configured according to required operating conditions. 6. Intelligent Inventory ManagementControl every pallet and storage location CC-WMS manages product information, quantities, locations, batches, and inventory movements while supporting configurable storage and inventory rules. 7. Automated Warehouse ControlCoordinate equipment and warehouse tasks YUNTU-WCS connects WMS instructions with automated equipment, coordinating task execution, equipment status, routing, and material movement. 8. Controlled Human AccessKeep routine operations away from hazardous storage areas By automating repetitive storage and retrieval tasks, the system can reduce unnecessary personnel entry into controlled storage zones while supporting site-specific safety procedures. |
| Technology | Application |
| Chemical Storage Racking | Provides designated and segregated pallet storage locations |
| Explosion-Protected Equipment | Supports operation in appropriately classified hazardous areas |
| Four-Way Shuttle System | Flexible high-density pallet storage and retrieval |
| Two-Way Pallet Shuttle | Deep-lane storage for high-volume chemical pallets |
| Six-Way Shuttle System | Flexible multi-directional storage for complex warehouse layouts |
| Stacker Crane ASRS | Automated high-bay pallet storage and retrieval |
| Conveyors & Lifts | Automated pallet transfer between warehouse zones |
| CC-WMS | Inventory, location, batch, and warehouse management |
| YUNTU-WCS | Equipment coordination, task execution, and warehouse control |
| Environmental Monitoring | Continuous monitoring of project-specific storage conditions |
| Safety & Access Systems | Support controlled warehouse operation and personnel safety |
Receiving → Identification → Inspection → Classification → Storage Zone Assignment → Automated Putaway → High-Density Storage → Environmental Monitoring → Automated Retrieval → Outbound Inspection → Dispatch
The workflow can be customized according to chemical category, packaging type, batch requirements, storage restrictions, environmental conditions, and applicable local regulations.
Chemical Raw Material WarehouseAutomated storage before production Manage raw materials by chemical category, batch, quantity, and production requirements while connecting storage with manufacturing operations. |
Finished Chemical Product WarehouseOrganized storage before shipment Automated storage helps manage finished products by SKU, batch, destination, and shipping priority. |
Flammable & Explosive Chemical StorageControlled storage with appropriate safety configuration Suitable equipment and storage configurations can be developed according to hazardous-area classification, chemical properties, and applicable safety requirements. |
Corrosive Chemical WarehouseDedicated storage for corrosive products Storage zones and handling equipment can be configured around chemical characteristics, packaging, compatibility, and leakage-control requirements. |
Chemical Distribution CenterHigh-density storage with automated retrieval Combine automated storage and warehouse software to manage large quantities of chemical products while improving inventory visibility and handling efficiency. |
Chemical Manufacturing WarehouseConnect materials, production, storage, and shipping Integrate raw-material storage, production-line supply, finished-goods storage, and outbound operations into a coordinated warehouse automation system. |
Safety-Oriented EngineeringDesign around chemical characteristics Zhuku considers chemical properties, storage compatibility, hazardous-area classification, environmental conditions, and operational requirements during system planning. |
Complete System IntegrationOne partner from design to implementation We integrate racking, shuttles, stacker cranes, conveyors, lifts, WMS, WCS, monitoring, and control systems into one coordinated solution. |
Flexible Automation TechnologiesChoose the right technology for the warehouse Different chemical warehouses can use different combinations of four-way shuttles, pallet shuttles, six-way shuttles, stacker cranes, conveyors, and lifts. |
Intelligent Warehouse ManagementConnect inventory data with physical operations CC-WMS and YUNTU-WCS provide the digital layer for inventory management, task execution, equipment coordination, and operational visibility. |
Customized Storage DesignBuilt around your actual project Storage density, pallet specifications, throughput, warehouse dimensions, environmental conditions, and chemical requirements determine the final system configuration. |
Global System Integration ExperienceEngineering for complex warehouse requirements Zhuku combines warehouse planning, automation equipment, software, system integration, installation, commissioning, and technical support. |
Your chemical warehouse requires more than storage capacity. It needs controlled segregation, appropriate safety configuration, environmental visibility, accurate inventory management, and reliable automated handling.
Send Zhuku your warehouse drawing, chemical categories, pallet specifications, storage capacity, environmental requirements, hazardous-area classification, and daily throughput. Our engineering team can evaluate your project and recommend a customized chemical warehouse storage solution.
Find answers to frequently asked questions about warehouse automation, system integration, equipment, installation, operation, maintenance, and after-sales support.

Zhuku is a trusted warehouse automation company providing system integration, intelligent storage solutions, automated warehouse systems, and warehouse racking for customers worldwide.